Food PackagingComponent AssemblyMachine
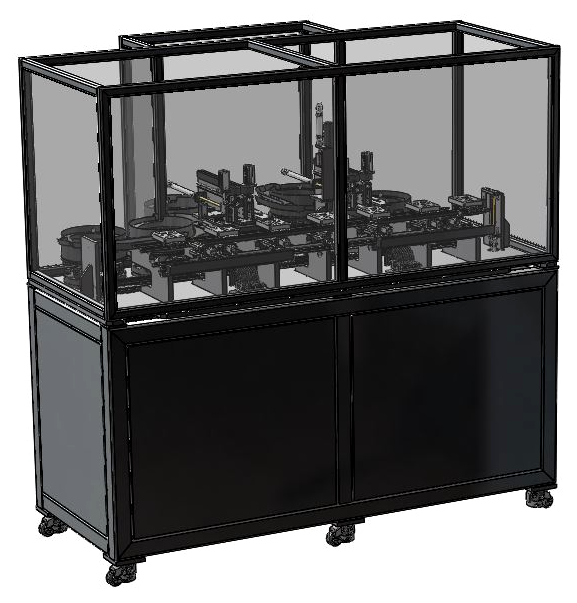
A compact guarded assembly platform combining vibratory bowl feeders, buffered part presentation, dedicated carriers and repeated handling stations around one controlled production datum.
Keep each station supplied and aligned
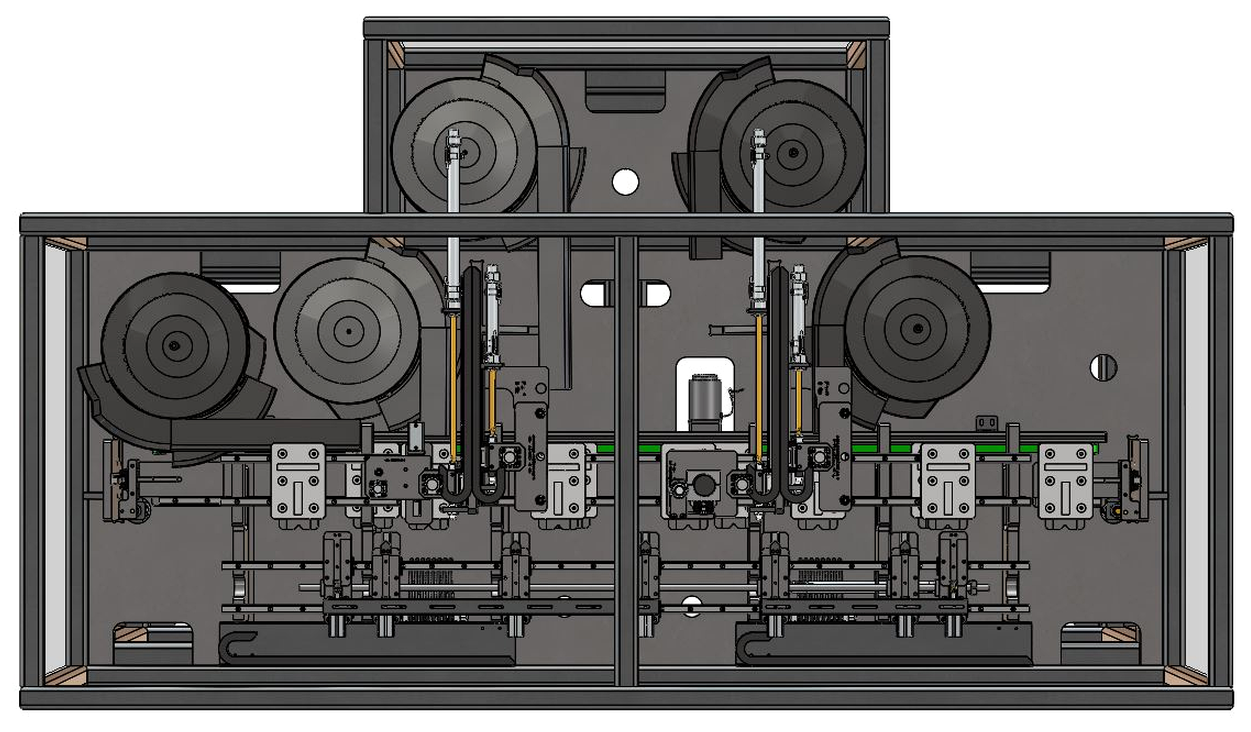
Different packaging components are oriented and presented by separate vibratory bowl feeders while a central carrier system moves the base component through the assembly sequence.
The main engineering challenge was to coordinate feeder output, buffer capacity, carrier motion and station dwell without losing the workpiece reference or starving downstream operations.
- Feeding
- Independent bowl feeders orient and present different components.
- Transfer
- The carrier path moves the base component through the repeated assembly sequence.
- Serviceability
- The machine layout retains access for adjustment, cleaning, feeder tuning and maintenance.
Carry the datum through the process
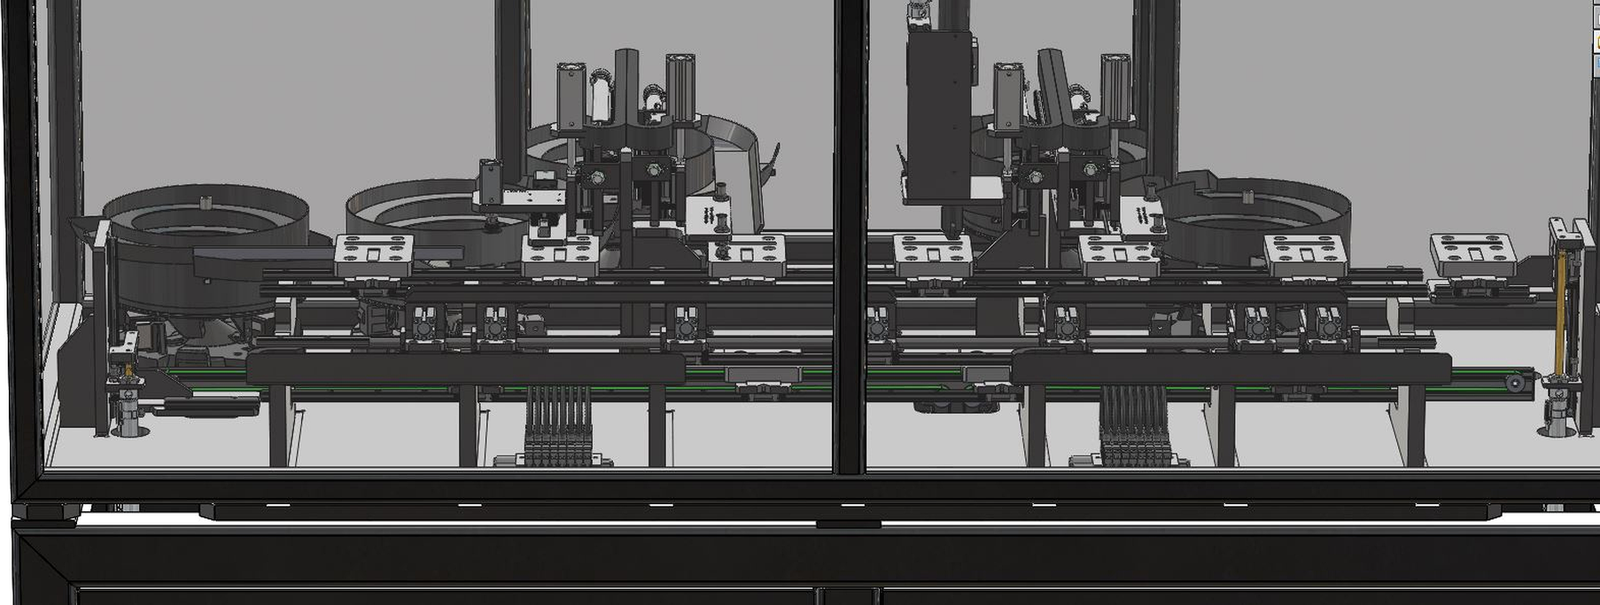
Dedicated nests maintain a consistent workpiece datum from station to station. Each feeder and handling module can then be tuned around its own component while the carrier system preserves the common process reference.
- Datum control
- Dedicated carriers maintain positive workpiece location through successive operations.
- Buffering
- Component presentation is separated from the carrier index so stations remain supplied.
- Coordination
- Feeding, transfer and assembly actions are organized around one repeatable reference.
Keep short motions close to the carrier
The repeated vertical handling modules use compact guided actuation suited to short stroke pick, place and seating actions. Keeping the active tooling close to the transfer line supports predictable station timing and a compact guarded envelope.
- Motion
- Compact guided actuation supports short pick, place and seating strokes.
- Packaging
- Repeated mechanisms are arranged within one guarded production platform.
- Maintainability
- Working and service spaces are retained around the feeder and station tooling.
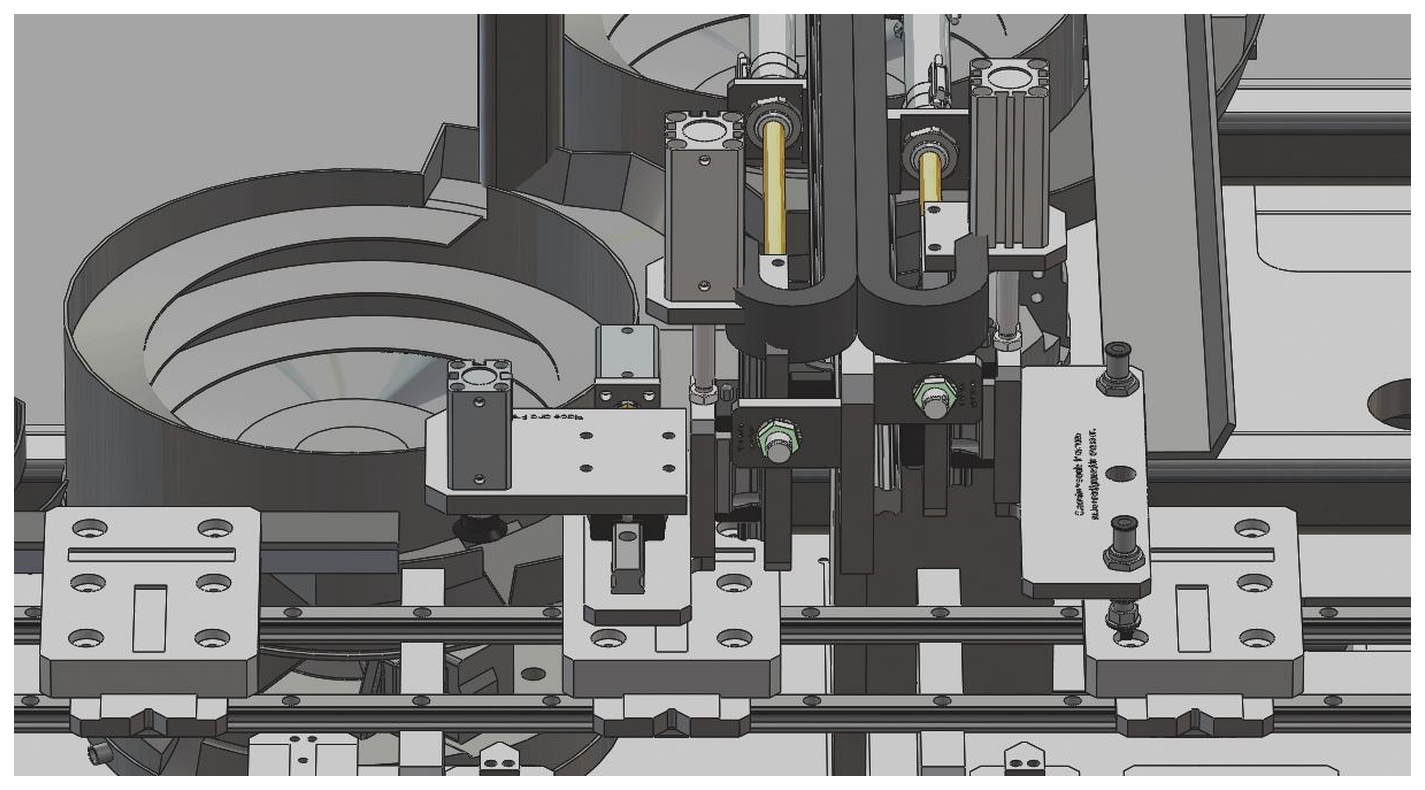
The machine met the required assembly rate
The completed machine achieved the intended production duty. The nominal output is linked directly to the carrier index interval, while the operating envelope accommodates component specific feeder behaviour, seating dwell and confirmation time.
Required production duty achieved.
One finished unit advanced per index at nominal duty.
Intended format and component dependent range achieved.
- Guarding
- The guarding and access philosophy was developed with reference to ISO 12100 and EN ISO 14120 principles.
- Packaging context
- The wider machine safety context references the EN 415 packaging machinery framework.
- Engineering scope
- Fabrixon scope covered the mechanical architecture, feeder integration, carrier transfer, pick and place modules, guarding and maintainability. Proprietary controls and product contact details are withheld.
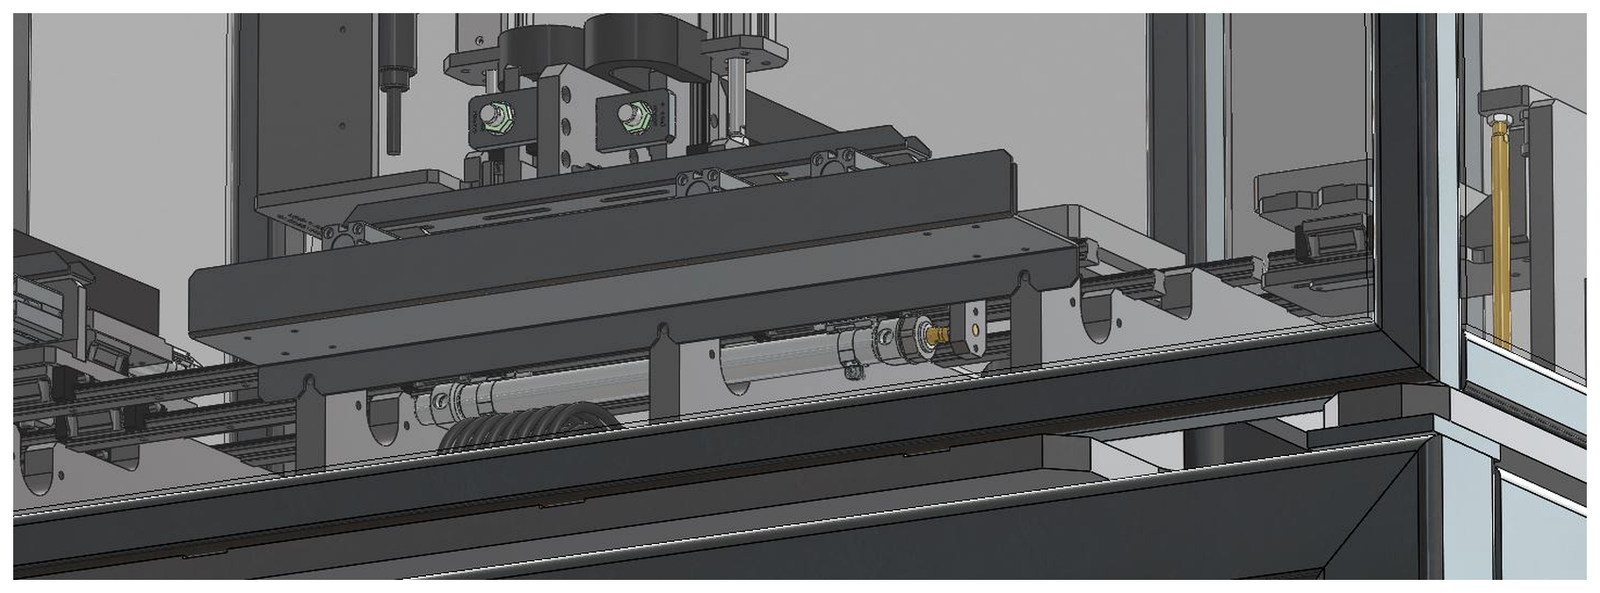
A common carrier datum made the multi station process controllable
The machine worked as one coordinated system because component feeding and repeated assembly motions were referenced back to the same carrier geometry instead of allowing each station to establish its own independent datum.
A coordinated assembly platform that achieved production duty
The completed machine integrated bulk feeding, component orientation, buffered presentation, carrier based datum control, repeated assembly stations and guarded packaging into one mechanical system. The successful application met the required nominal output and intended operating envelope.
- Performance
- Nominal production duty of approximately 45 assembled units/min was achieved.
- Process control
- Carrier based datum control maintained the workpiece reference through successive stations.
- Machine integration
- Feeding, transfer, repeated handling and guarding were resolved as one coordinated platform.
- Project result
- The machine successfully delivered the intended multi component assembly process.